Foreword
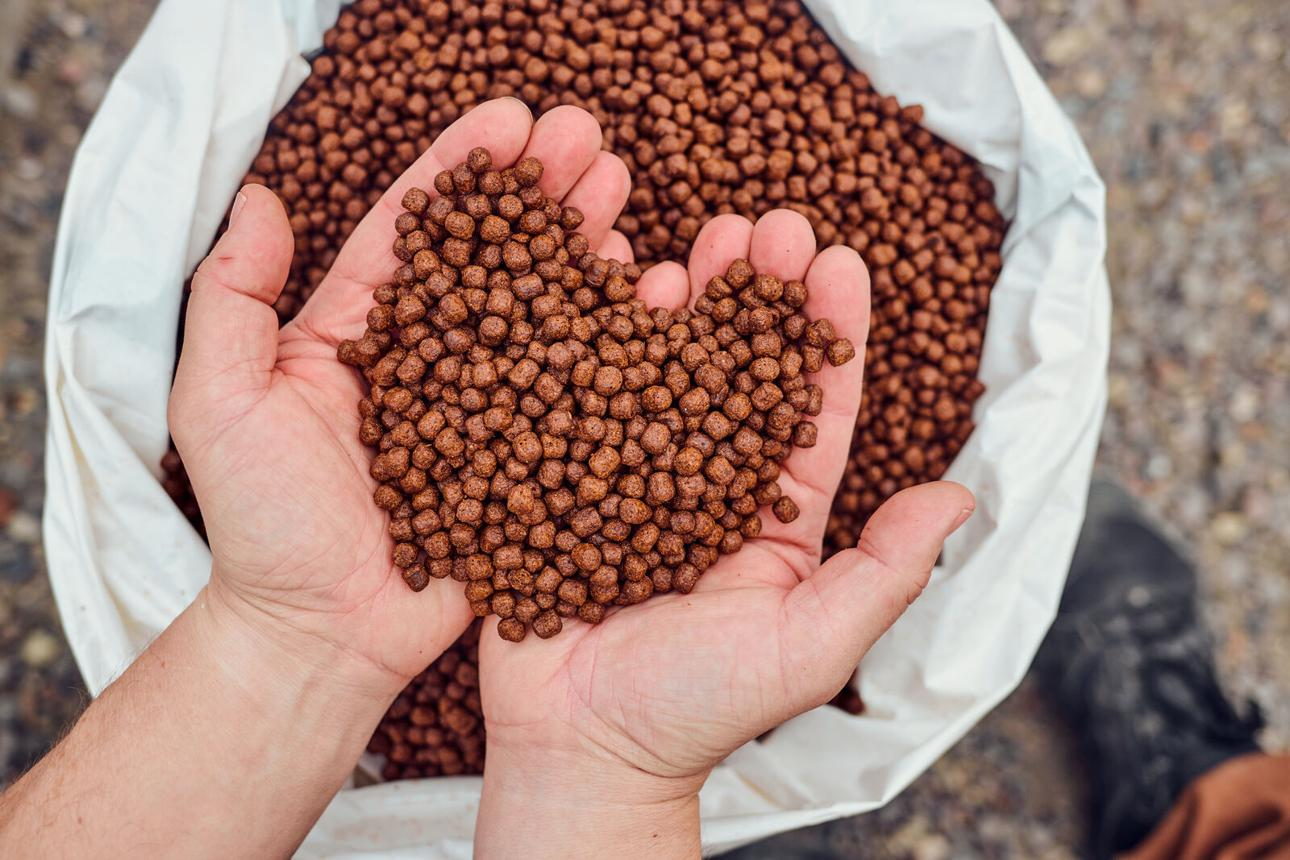
Fish fry feed with a particle size of <0.3 mm serves as an “initial” or “starter” diet for larval and juvenile fish, designed for those with very small mouth openings. This type of feed demands rigorous standards regarding the ultra-fine grinding of raw materials, material rheology, granulation, particle size classification, water stability, and the preservation of heat-sensitive active ingredients. Conventional ring-die pelleting is generally incapable of producing finished particles smaller than 0.3 mm. Current mainstream production methods include: extrusion followed by crushing and screening; micro-extrusion; and micro-encapsulation. This article examines the entire production process—covering raw material pretreatment, conditioning, granulation, drying and cooling, post-processing (coating), screening and classification, quality metrics, common operational challenges, and optimization strategies—to provide a technical reference for industrial-scale production.
I. Process Challenges
1. Difficulty in Granulation: The extremely small die-hole diameter leads to high back pressure, making the dies highly prone to clogging. This necessitates precise control over the rheological properties of the material. Most standard extruders have a minimum die-hole diameter of 0.6 mm or larger, rendering them unsuitable for the direct extrusion of particles <0.3 mm.
2. Stringent Grinding Requirements: To prevent die clogging, deformed particles, and excessive fines, the largest particles in the raw material must not exceed one-third of the target finished particle size.
3. Loss of Heat-Sensitive Nutrients: Ingredients such as fish meal, hydrolyzed proteins, vitamins, and enzymes are susceptible to degradation at high temperatures. Furthermore, because fine materials facilitate rapid heat transfer, they are prone to overheating and subsequent loss of biological activity during the drying and extrusion processes.
4. Trade-off Between Particle Strength and Water Stability: Due to their minute size, these particles often lack sufficient mechanical strength, making them highly susceptible to breakage during transport and screening. Once in water, they may disintegrate or dissolve too rapidly, leading to water pollution and inadequate feed intake by the fish fry.
5. Difficulty in Controlling Particle Size Uniformity: Crushing processes often generate significant amounts of fine dust. Additionally, achieving precise screening and classification is challenging; a broad particle size distribution can negatively affect the selective feeding behavior of the fish fry.
II. Comparison of Mainstream Processing Routes
Route A: Twin-screw extrusion, crushing, and screening (most common in industrial production)
Process: Raw material intake → ultrafine grinding → ingredient mixing → conditioning → twin-screw extrusion → production of coarse granules (0.8–1.2 mm) → drying → cooling → low-speed crushing → multi-stage precision screening → coating → finished product (<0.3 mm)
Advantages: Mature equipment, high production capacity, thorough starch gelatinization, high digestibility; capable of producing floating or slow-sinking feed; avoids the issue of clogging in ultra-small orifice dies.
Disadvantages: Crushing generates a significant amount of fine powder, resulting in a broad particle size distribution; requires multi-stage screening, leading to a relatively low yield of the final product.
Route B: Direct micro-extrusion granulation (for high-end fry/larval feed)
Process: Ultrafine grinding → ingredient mixing → precise, zone-based conditioning → twin-screw micro-extrusion (using specialized micro-orifice dies and high-speed synchronous cutting) → low-temperature fluidized-bed drying → coating → finished product (<0.3 mm)
Advantages: Granules are formed directly, resulting in a uniform, rounded shape, narrow particle size distribution, and minimal dust; excellent water stability. Disadvantages: High capital investment for equipment; extremely high precision requirements for die manufacturing; high risk of die orifice clogging; low production capacity; highly sensitive to formulation, grinding, and conditioning parameters.
Route C: Microencapsulation process
Nutritional components are emulsified and encapsulated, then granulated via spray drying to produce micro-particles.
Advantages: Particle size can be reduced to the scale of tens of microns; provides effective protection for heat-sensitive substances.
Disadvantages: Very high costs and low output; primarily used in laboratory settings or for high-end, specialized fry/larval feeds; rarely adopted by large-scale commercial feed mills.
In domestic industrial practice, the vast majority of feed manufacturers in China prefer the extrusion-crushing-multi-stage screening process for producing fish fry/larval feed with a particle size of <0.3 mm.
III. Research on Process Parameters for Key Operations
3.1 Raw Material Pretreatment: Ultrafine Grinding
1. Grinding Equipment: Air-classifying mill or variable-frequency ultrafine pulverizer; standard hammer mills cannot achieve the required fineness.
2. Particle Size Control: 90% of the raw material must pass through a 200-mesh sieve, with a maximum particle size of ≤80 μm. The maximum particle size of the raw material should be ≤1/3 of the final product’s particle size to prevent die clogging and pellet defects.
3. Temperature Control: The temperature within the grinding chamber must be ≤35°C to minimize the thermal degradation of heat-sensitive components such as lysine and vitamin C. Highly active protein-based raw materials require low-temperature grinding.
4. Mixing: The coefficient of variation (CV) for the mixture must be ≤5% to ensure the uniform distribution of trace elements and palatability enhancers, thereby preventing nutritional segregation.
3.2 Conditioning
Utilize a dual-shaft differential conditioner for zoned conditioning:
1. Conditioning Temperature: 90–100°C; conditioning duration: 3–6 minutes.
2. Moisture Content After Conditioning: 20–22%; this ensures sufficient starch gelatinization, improves material plasticity, and reduces the likelihood of die wear and clogging in the extruder.
If moisture is too low, the material lacks plasticity, resulting in fragile pellets; if moisture is too high, it increases the load on the subsequent drying stage and causes pellets to stick together.
3.3 Extrusion
(1) Extrusion and Crushing Process (for producing 0.8–1.2 mm intermediate-sized pellets)
a. Equipment: Twin-screw extruder; screw compression ratio ≥1:3.2.
b. Barrel Temperature: 85–95°C in the feed section, 105–120°C in the melting section, and 95–105°C in the discharge section. A High-Temperature Short-Time (HTST) process is employed to minimize the destruction of heat-sensitive nutrients.
c. Screw speed: 220–280 rpm; adjusted based on material rheology to ensure a homogeneous melt. d. Die orifice diameter: 0.8–1.2 mm; high-speed synchronous cutting produces uniform, short, extruded pellets.
(2) Micro-direct extrusion process (targeting a final product size of <0.3 mm)
Die orifice diameter: 0.25–0.3 mm, with a machining tolerance of ≤0.05 mm. Equipped with a vacuum-assisted cutting system to minimize post-extrusion expansion and reduce pellet tearing or the formation of burrs. This process requires strict control over the starch content in the formulation and the rheological stability of the material.
3.4 Drying and Cooling
The moisture content of the extrudate is 18%–22%.
1. Low-temperature drying in a fluidized bed is preferred, using a multi-stage gradient drying process (60–70°C) to prevent localized overheating. Rapid, high-temperature drying is not recommended, as it induces high internal stress, leading to cracking and a sharp increase in the rate of powder formation (fines).
2. Final product moisture content: 8.0%–10.0%. 3. Cool to near room temperature to reduce pellet brittleness, preparing the material for subsequent size reduction (crushing).
3.5 Crushing and Multi-stage Screening (Core Process in the Extrusion-Crushing Route)
1. Crushing: Use a low-speed toothed-roll crusher; high-speed hammer-mill crushing is prohibited. This minimizes over-pulverization and the generation of ultra-fine dust. The roll gap should be fine-tuned based on the target particle size.
2. Multi-stage screening: Equipped with multi-layer precision grading screens featuring mesh apertures of 0.3 mm, 0.25 mm, and 0.18 mm. Material retained on the screens (>0.3 mm) is returned for further crushing, while material between 0.18 mm and 0.30 mm constitutes the target finished product.
1. Fine particles (<0.18 mm) that pass through the screens are recycled back into the raw material mix to increase yield.
Challenge: The yield of finished products from crushing and screening processes is typically only 55%–70%. Recycling fine particles alters the actual starch-to-protein ratio of the formulation, requiring the production facility to strictly control the recycling ratio.
3.6 Post-production spray coating (crucial for enhancing water stability)
Due to their large specific surface area, small-sized particles tend to lose nutrients rapidly when submerged in water.
1. Following the cooling stage, a negative-pressure atomized spray is applied—consisting of fish oil and soybean lecithin, potentially combined with bile acids or sustained-release coating agents—to form a hydrophobic protective film on the surface of the particles.
2. The oil application rate is 2%–4%; the process is conducted at low temperatures to prevent lipid oxidation and particle adhesion.
3. After coating, the product undergoes a second, mild cooling phase followed by screening to remove any particles that have clumped together due to the coating process.
IV. Key Quality Control Indicators (Feed for Fish Fry <0.3 mm)
Table
| Testing Item | Control Reference Value | Description |
| Particle Size Distribution | 0.18–0.30 mm: ≥85% | Measured by sieve analysis |
| Moisture Content | 8–10% | Prevents caking and mold growth during storage |
| Pellet Hardness | 8–15 N | Excessive hardness makes pellets difficult for fry to digest; insufficient hardness makes them prone to breaking during transportation |
| Fines Rate | ≤8% | Measured by the tumbling box method; reflects the pellets’ resistance to breakage during production and transportation |
| Water Stability | Weight loss ≤12% after 15 minutes of immersion | Reduces nutrient leaching and water pollution |
| Starch Gelatinization Degree | ≥85% | Determines digestibility and pellet bonding strength |
V. Common Process Issues and Optimization Strategies
1. Frequent Die Hole Clogging (Direct Extrusion Process): Causes include insufficient raw material pulverization, low moisture during conditioning, unstable material rheology, or poor precision of die holes. Strategies: Ensure strict control over ultra-fine grinding; stabilize moisture and temperature during conditioning; regularly clean and polish the die.
2. High Fines Content/Crumbling in Finished Product (Crushing & Screening Process): Causes include excessive crushing roller speed, insufficient starch gelatinization during extrusion, or high internal stress due to excessive drying temperatures. Strategies: Reduce crushing roller speed; increase starch gelatinization; employ multi-stage low-temperature fluidized-bed drying; apply surface coating.
3. Rapid Disintegration and High Nutrient Leaching in Water: Causes include insufficient gelatinization, lack of a hydrophobic coating, or excessive internal porosity. Strategies: Optimize conditioning and extrusion parameters to improve gelatinization; apply a hydrophobic coating (e.g., atomized phospholipids or fats).
4. Wide Particle Size Distribution (Mixed Large and Small Particles): Strategies: Implement multi-stage precision screening; ensure stable recycling/re-incorporation of fine particles; precisely adjust the gap between crushing rollers. 5. Strategies to mitigate the loss of heat-sensitive nutrients: Utilize low-temperature grinding for raw materials; employ high-temperature, short-time (HTST) extrusion; and apply vitamins and enzyme preparations via post-extrusion spraying rather than including them in the primary extrusion process.
VI. Interactive Effects of Formulation on Processing Technology
1. Starch serves as the primary binding agent, typically comprising 18–24% of the formulation. Insufficient starch results in poor pellet durability and high rates of fines (dust), while excessive starch leads to overly hard pellets, which impose a digestive burden on fish fry.
2. High-protein ingredients (such as fish meal or hydrolyzed proteins) alter the viscosity of the material, which can cause fluctuations in die pressure; this necessitates finer grinding of the raw materials.
3. The oil content prior to extrusion should be kept low (≤3–4%), as higher levels weaken pellet cohesion. The bulk of the oil should be applied via post-extrusion spraying.
VII. Summary and Outlook
For fish fry feed with a particle size of <0.3 mm, direct micro-extrusion yields pellets with excellent physical form; however, this approach requires specialized, high-cost equipment and is limited in production capacity. For domestic feed manufacturers, an “extrusion–crushing–multi-stage screening” process is better suited for large-scale production. Key control points include: ultra-fine grinding of raw materials; ensuring thorough starch gelatinization during conditioning and extrusion; utilizing low-speed crushing to minimize the generation of excessive fines; employing multi-stage precision classification; and applying oil and phospholipids as a post-extrusion coating to enhance water stability.
Future developments should focus on: designing specialized micro-dies, implementing real-time in-line particle size monitoring, and adopting low-damage crushing technologies to improve the yield of finished products. Furthermore, the use of post-extrusion micro-encapsulation (coating) techniques will help better balance pellet durability, water stability, and nutrient release—ultimately supporting both efficient digestion and absorption in fish fry while minimizing the environmental impact on the aquaculture water body.